In high-pressure flight control and propulsion systems, defects invisible to the naked eye can ruin your project. For engineers and quality auditors, the most challenging issues are the "invisible killers"-tiny cracks, inclusions, and voids hidden deep within the pipe walls.
At Gnee Alloy, we eliminate these risks. Our 100% non-destructive testing (NDT) inspection process ensures that every meter of pipe delivered meets the highest aerospace-grade integrity standards.
Click to get an Inconel 625 product quote
Understanding 100% Ultrasonic and Eddy Current Testing for AMS 5581 Tubing

Understanding 100% Ultrasonic and Eddy Current Testing for AMS 5581 Tubing
The AMS 5581 standard specifies seamless or welded corrosion-resistant and heat-resistant nickel alloy tubing (such as Inconel 625) for use in high-stress aerospace fluid systems. This standard mandates 100% ultrasonic testing (UT) and eddy current testing (ECT) to ensure the overall structural integrity of the tubing and to detect even minute internal, external, or through-wall defects.
What is Alloy 625?
Alloy 625 (commonly known as Inconel 625) is a high-quality nickel-chromium-molybdenum superalloy. Due to its exceptional strength, excellent machinability, and superior water resistance and high-temperature oxidation resistance, it is highly favored in high-stress, corrosive environments.

1. AMS 5581 tube chemical composition (wt%)
| Element | Content (%) | AMS 5581 Requirement | Function |
|---|---|---|---|
| Nickel (Ni) | ≥ 58.0 (Balance) | ≥ 58.0 | Matrix element; corrosion resistance and high-temperature stability |
| Chromium (Cr) | 20.0 – 23.0 | 20.0 – 23.0 | Oxidation and corrosion resistance |
| Molybdenum (Mo) | 8.0 – 10.0 | 8.0 – 10.0 | Core element – provides pitting and crevice corrosion resistance |
| Niobium (Nb) | 3.15 – 4.15 | 3.15 – 4.15 | Solid-solution strengthening; carbide stabilizer |
| Iron (Fe) | ≤ 5.0 | ≤ 5.0 | Residual element |
| Titanium (Ti) | ≤ 0.40 | ≤ 0.40 | Supplementary strengthening |
| Aluminum (Al) | ≤ 0.40 | ≤ 0.40 | Supplementary strengthening |
| Carbon (C) | ≤ 0.10 | ≤ 0.10 | Low carbon for weldability and corrosion resistance |
| Manganese (Mn) | ≤ 0.50 | ≤ 0.50 | Deoxidizer |
| Silicon (Si) | ≤ 0.50 | ≤ 0.50 | Deoxidizer |
| Phosphorus (P) | ≤ 0.010 | ≤ 0.015 | Stricter for aerospace – ensures toughness |
| Sulfur (S) | ≤ 0.005 | ≤ 0.015 | Stricter for aerospace – ensures hot workability |
| Cobalt (Co) | ≤ 1.0 | ≤ 1.0 | Residual element |
2. Our 100% Non-Destructive Testing at Gnee Alloy

A. Ultrasonic Testing (UT)
Method: High-frequency acoustic waves scan the entire volume of the pipe wall.
Objective: Detects longitudinal and transverse defects, internal voids, and variations in wall thickness.
Benefits: Ensures a 100% dense pipe matrix, free from the "spots" or pores commonly found in standard commercial alloys.
B. Eddy Current Testing (ET)
Method: Electromagnetic induction detects surface and subsurface defects.
Objective: Identifies minute overlaps, pits, and seams that are difficult to detect visually.
Benefits: Guarantees a zero-defect surface finish, maximizing material lifespan under fluctuating thermal stress.

3. Gnee Alloy Technical Inspection
| Inspection Category | Standard / Protocol | Acceptance Criteria | Buyer Value |
| Internal Integrity | UT (AMS 2154 Class A) | Zero Linear Indications | Elite pressure containment. |
| Surface Integrity | ET (ASTM E426) | Zero Surface Defects | Prevents crack initiation. |
| Pressure Safety | Hydrostatic Test | 1.5x Operating Pressure | Zero-Leakage Guarantee. |
| Microstructure | Metallographic (ASTM E112) | Level 8 Grain or Finer | Maximized Fatigue Life. |
| Traceability | MTC 3.1 / 3.2 | Full Heat Analysis | Audit-Ready Compliance. |
4. Gnee Alloy AMS 5581 Pipe Specialty
Every tube we ship is a documented asset. We provide total transparency through our MTC 3.1 Traceability system:
Heat Number Identity: Every tube is heat-number stamped and matched to its original vacuum melt.
Verified Standards: Documentation proves compliance with AMS 5581, AMS 5599, and ASTM B444.
Digital Audit Trail: We maintain NDT records for up to 10 years to support your future safety audits.
5. AMS 5581 tube quality certification (MTR requirements)
| Document | Required Information |
|---|---|
| Heat Number | Full traceability to melt |
| Melting Process | VIM + VAR certification |
| Chemical Composition | Full analysis (Ni, Cr, Mo, Nb, Fe, Ti, Al, C, Mn, Si, P, S, Co, O, N, H, Pb, Bi) |
| Mechanical Properties | UTS, YS, Elongation, Hardness |
| Dimensional Inspection | OD, wall thickness, length, straightness |
| Surface Finish | Surface condition and Ra value |
| NDT Results | 100% ET + 100% UT + Hydrostatic test report |
| Flattening Test | Pass/fail |
| Flaring Test | Pass/fail |
| Heat Treatment Record | Solution annealing parameters |
| Certification Type | EN 10204 Type 3.2 (mandatory) |
Why Choose Gnee as Your Nickel-Based Alloy Supplier
✅️Direct Factory Price: Eliminate markups from trading agents who don't perform in-house testing.
✅️Industrial Durability: Our testing protocols ensure your components withstand extreme vibration and temperatures up to 800°C.
✅️Risk Mitigation: Reduce your scrap rate during assembly by starting with 100% verified material.
✅️Global Logistics: Secure packaging to maintain surface integrity during transit to the USA, Europe, and Asia.
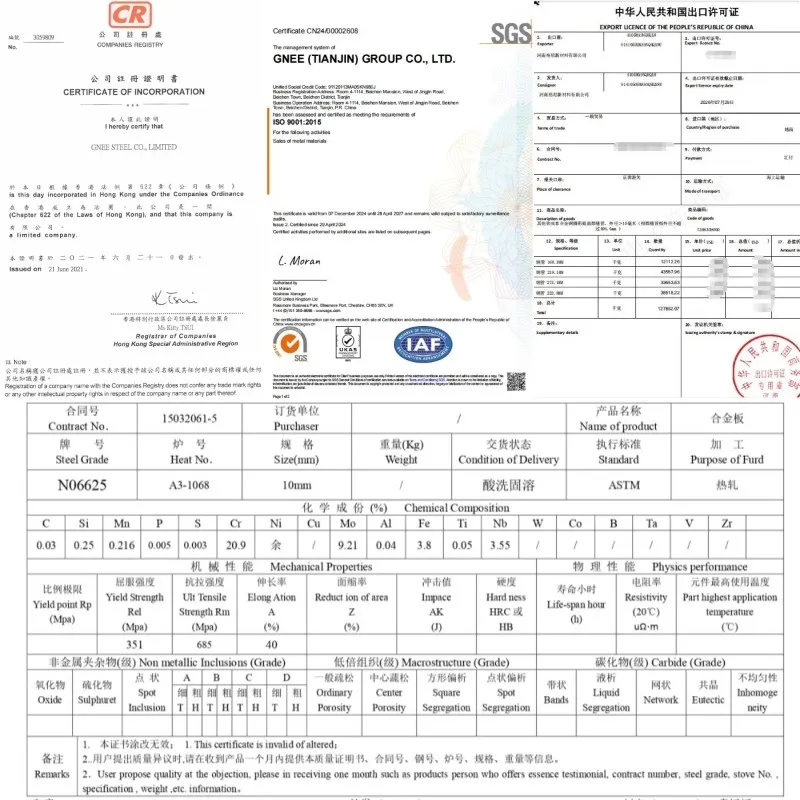
Gnee Alloy Inconel 625 Certificate
📦 Packaging and Shipping
All Nickel Based Alloy products are packaged using the following methods:
Wooden pallets or crates
Moisture-proof packaging
Labels with furnace number, standard, and size labels
Shipped worldwide by sea, air, or express
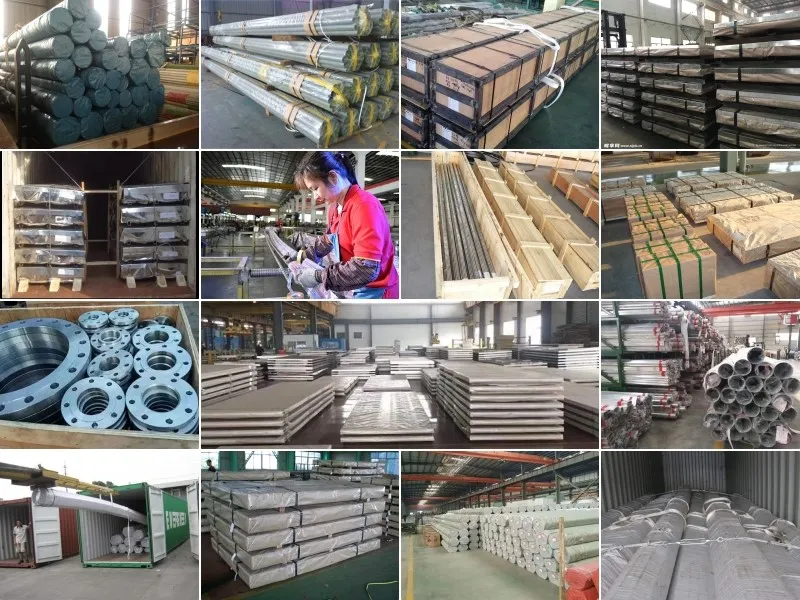
Gnee Alloy Alloy 625 Product Packing
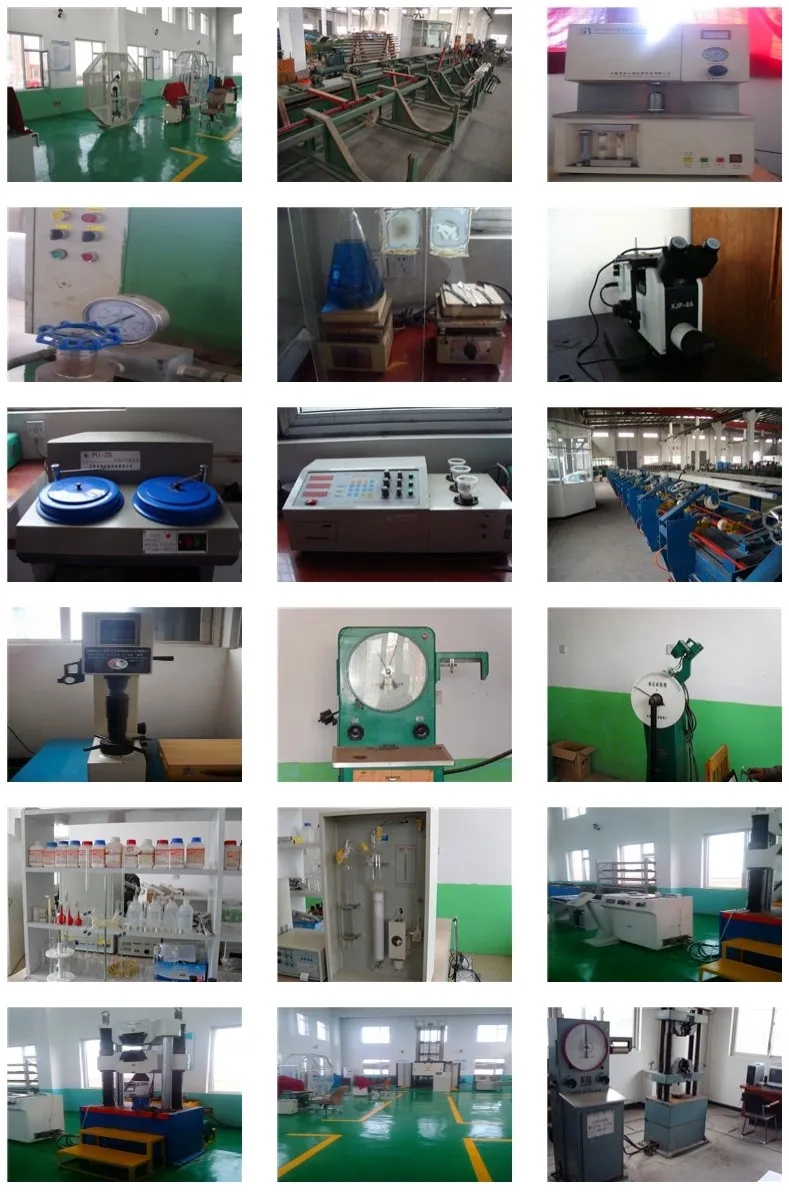
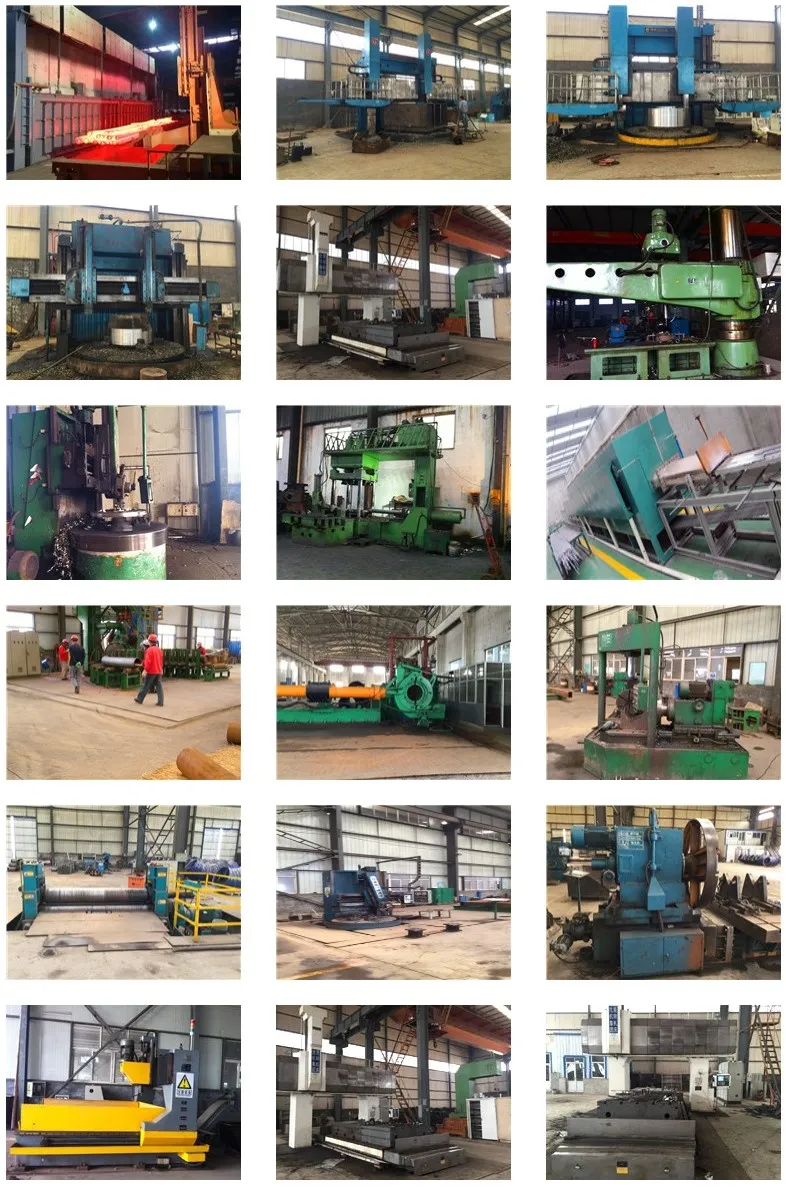
⚒️Gnee Alloy Production Line Equipment and Product Testing
Contact us for the latest export price quote for 625 Alloy
FAQ
Q1: Why is UT mandatory for Inconel 625 fuel lines?
A: Inconel 625 is subject to high-vibration engine environments. Even a microscopic internal inclusion can trigger High-Cycle Fatigue (HCF) cracking. UT is the only way to verify the material is "clean" enough for flight safety.
Q2: Does 100% NDT testing increase the lead time?
A: As a Specialized Manufacturer, we perform NDT in-line. While it adds a layer of precision, we maintain a massive Wholesale Inventory to ensure Short Lead Times on standard aerospace sizes.
Q3: Is your material compliant with Nadcap standards?
A: Yes. Our melting and testing processes are ready for Nadcap and AS9100 audits, serving as a Reliable Supplier for global Tier-1 aerospace OEMs.
Q4: Can I request MTC 3.2 certification with third-party witnessing?
A: Absolutely. We frequently host inspectors from SGS, TUV, and Lloyd's Register to witness our UT and tensile testing before material release.